Tooling for non-ferrous pressure die casting
Tooling that runs right the first time
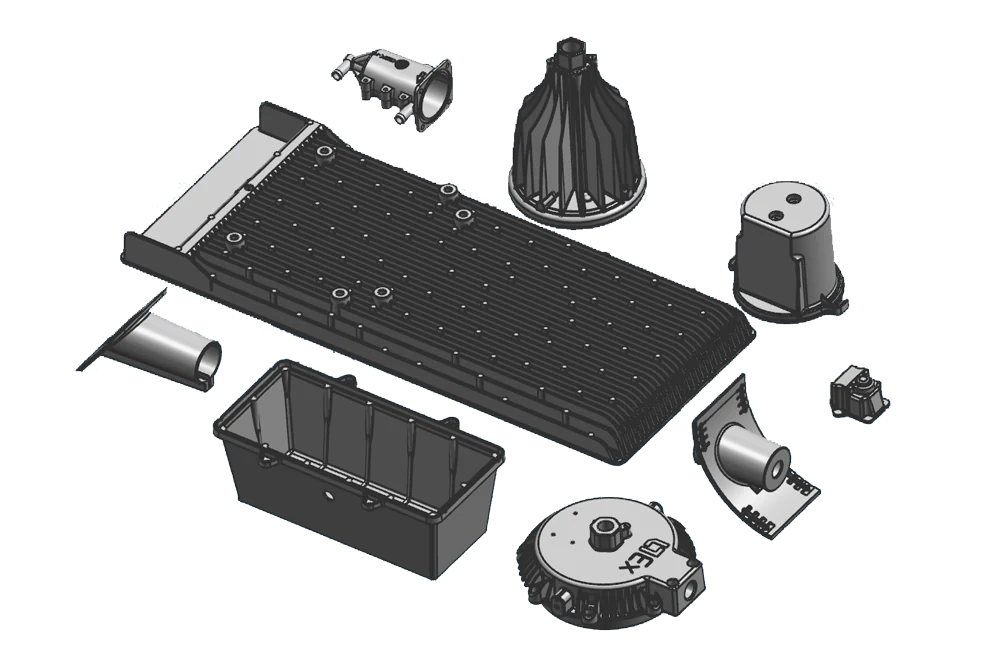
I design high pressure die casting moulds, trim dies and gravity dies for aluminium alloys. You receive a package that can be manufactured and put straight into production — no rework on the shop floor.
- 40
- years designing casting tooling
- 200+
- completed tooling projects
- 18
- recurring clients
- 1994
- CAD/CAM training at EDS, Cologne
What I design
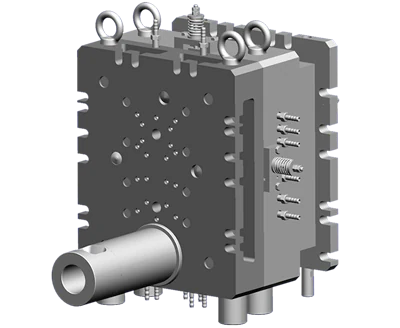
High pressure die casting moulds
Single and multi-cavity moulds for aluminium alloys, with slides, hydraulic cores, thermal control and vacuum systems.
More →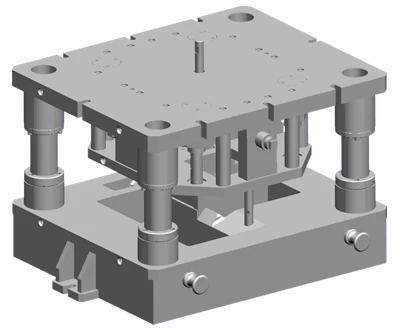
Trim dies
Trimming of gates, flash and overflows on die cast parts. Designed together with the mould so the part locates precisely.
More →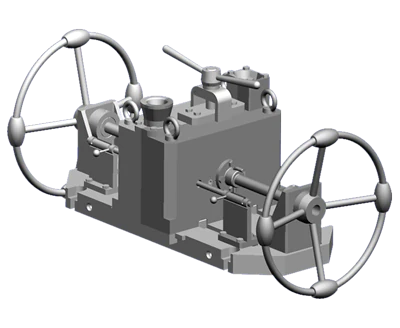
Permanent moulds
Machine and manual gravity dies for non-ferrous alloys, where volumes do not justify a die casting mould.
More →Why the designer decides more than the machine
A mistake in the tooling design does not show up on the drawing. It shows up at launch, when the metal is already in and the mould is in the machine.
- 01
The tooling cannot be made
The design does not suit the machines on your floor: features that cannot be cut, mechanisms that cannot be built.
- 02
The part comes out defective
Porosity, short shots, cold shuts, gas cavities, geometry drifting out of tolerance.
- 03
Rework costs
A failed launch means rebuilding the mould — comparable in money to a new project.
- 04
Missed production dates
While the tool is being corrected nothing is produced, and commitments to your own customer are already made.
- 05
Short tool life
The mould survives few shots and goes for repair long before it should.
Work
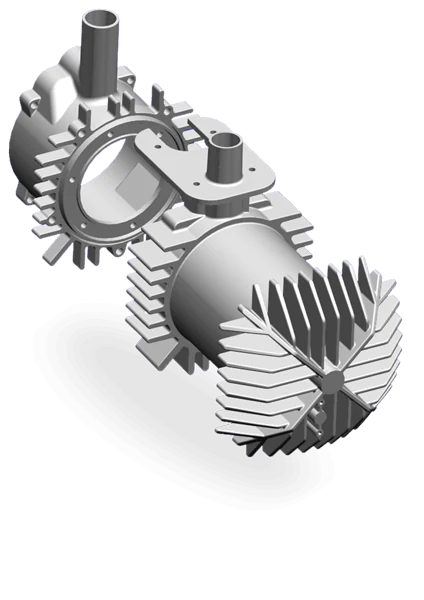
Heat exchanger housing with adapter
Heat exchanger for an automotive pre-heater. Two moulds, each with two parting directions.
- Tooling
- 2 die casting moulds
- Slides
- 3
- Lead time
- 6 wk
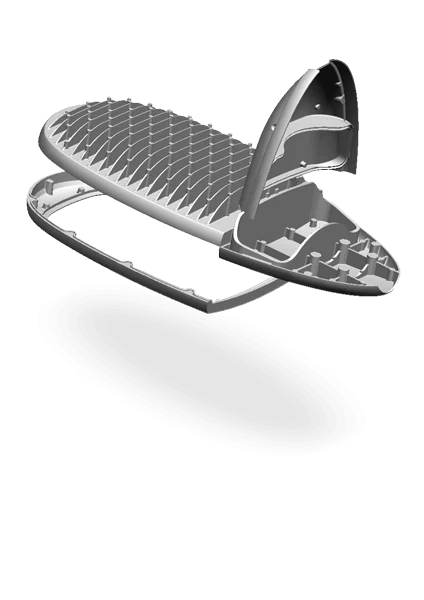
LED street light housing, 740×310 mm
Housing for a street luminaire mounted on lighting columns. Three moulds, each suited to a different casting machine.
- Tooling
- 3 die casting moulds
- Lead time
- 6 wk
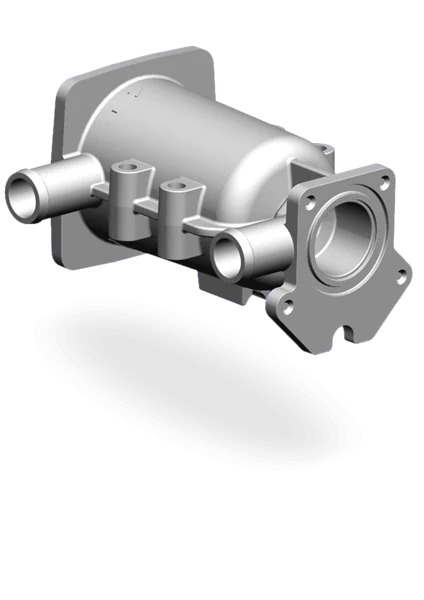
Engine pre-heater housing
Single-cavity mould with a slide travelling more than 100 mm on a purpose-built mechanism.
- Tooling
- Die casting mould
- Slides
- 3
- Lead time
- 4 wk

Armrest with bracket for high-speed trains
The castings themselves were redesigned first, then two moulds were designed.
- Tooling
- 2 die casting moulds + part redesign
- Lead time
- 8 wk
What you receive
Documentation to your standard
Assembly and detail drawings, specifications and bought-out part lists. Drawings are normally issued to ESKD, the Russian equivalent of ISO drawing practice; where a project requires ISO or a customer standard, the package is prepared accordingly.
Native NX files
I work in Siemens NX (Unigraphics) and deliver native .prt files alongside STEP — not geometry converted twice on the way to your tool room. My CAD/CAM training was at EDS in Cologne in 1994, with the company that owned Unigraphics.
Correspondence in English. NDA on request. Time zone UTC+4.
Who I work with
Plants that have mastered and now produce parts from tooling I designed.


Send the part — get a price and a schedule
Request a quote
Attach a 3D model or a drawing of the part and tell me which machine it runs on. Within 24 hours you get a fixed price, a delivery date and a draft contract.
- What I need
- 3D model or drawing of the part
- Die casting machine type
- Alloy and annual volume